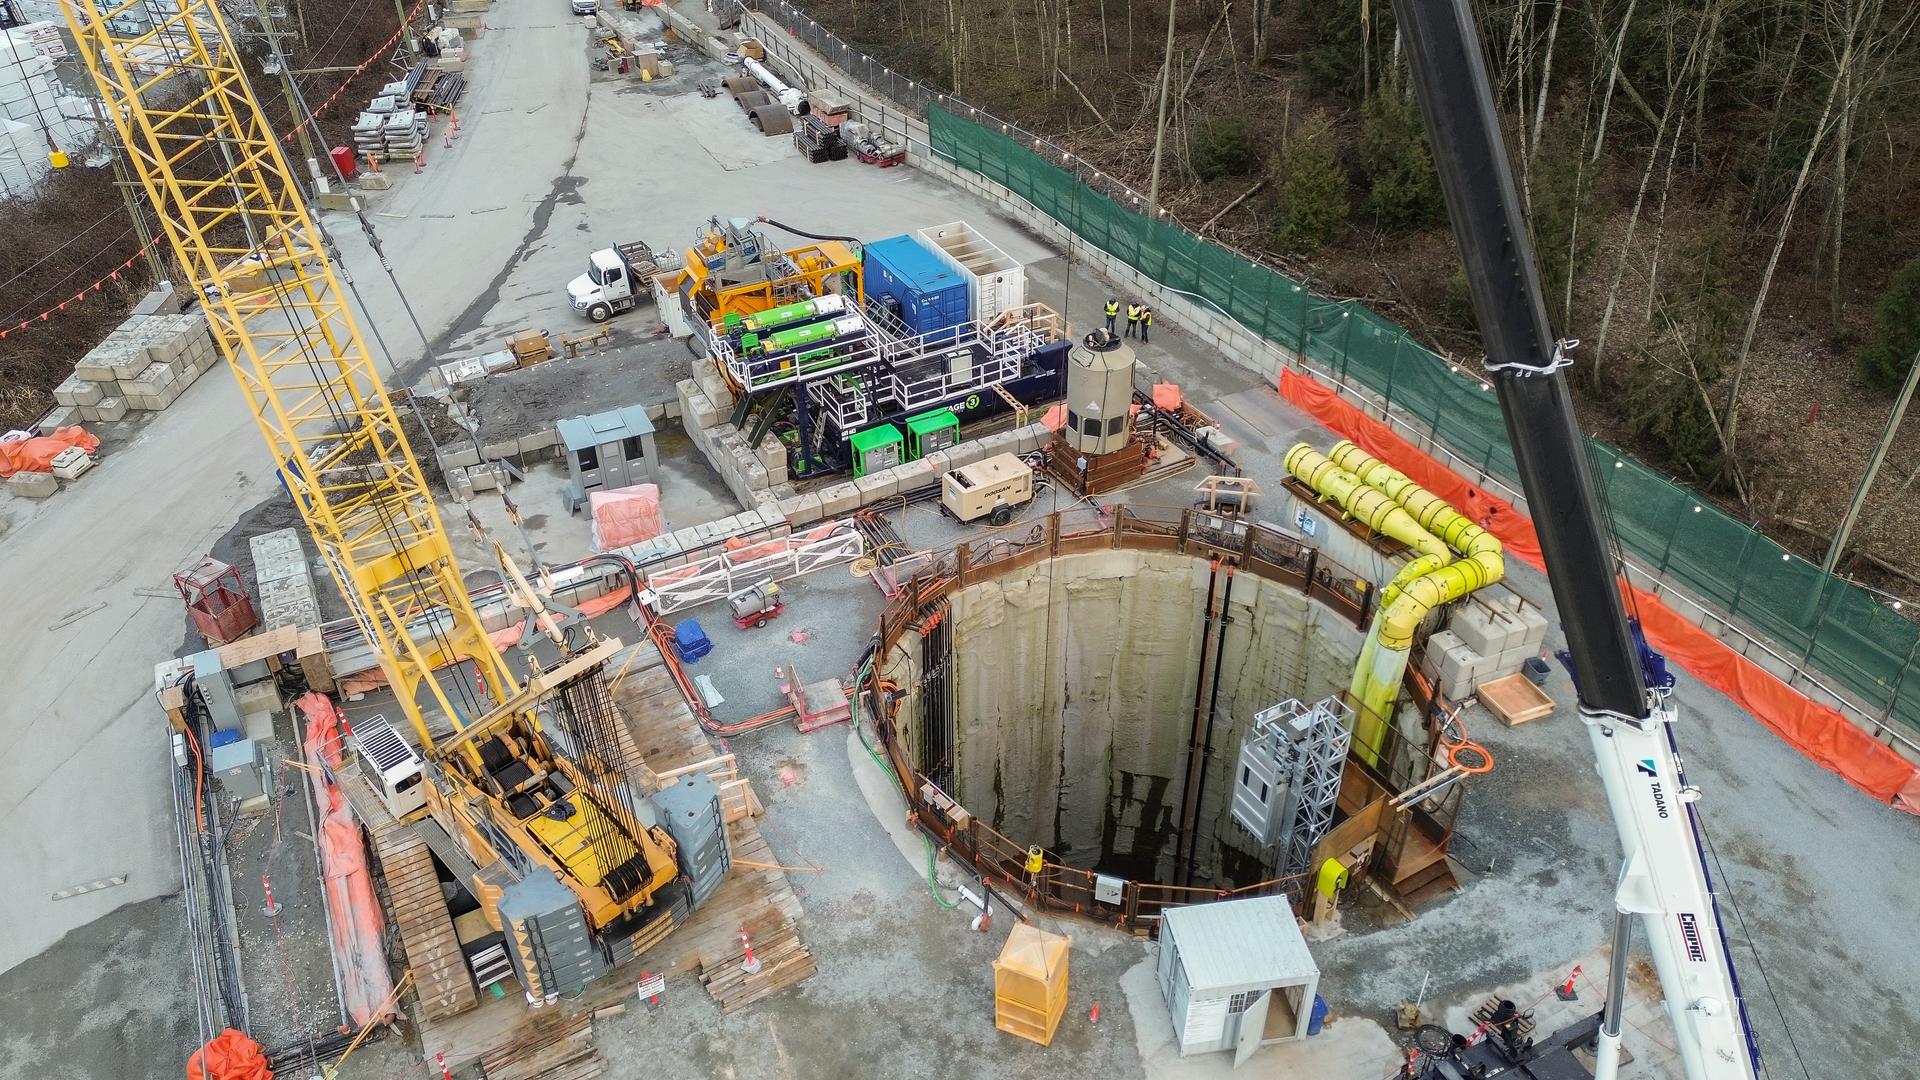
Two plants combine into a BE 600-C for up to 600 m³/h.
Slurry separation for tunnelling, microtunnelling and HDD
S3S keeps slurry TBM, microtunnelling, and HDD operations moving by separating excavated solids from drilling fluid at the surface, recovering fluid for reuse and producing stackable spoil for efficient hauling and disposal.
The BE-300 slurry treatment plant
Screen out coarse solids and remove sand from construction and tunnelling slurry.
Using 20-inch desanding cyclones and 6-inch desilting cyclones.
Gravel and large pieces come out first, before the slurry reaches the cones.
Tunnelling and trenchless work we support
Separation capacity keeps excavation moving. S3S sizes your plant to match slurry flow and anticipated ground conditions, preventing solids buildup from becoming a production bottleneck.
TBM slurry separation
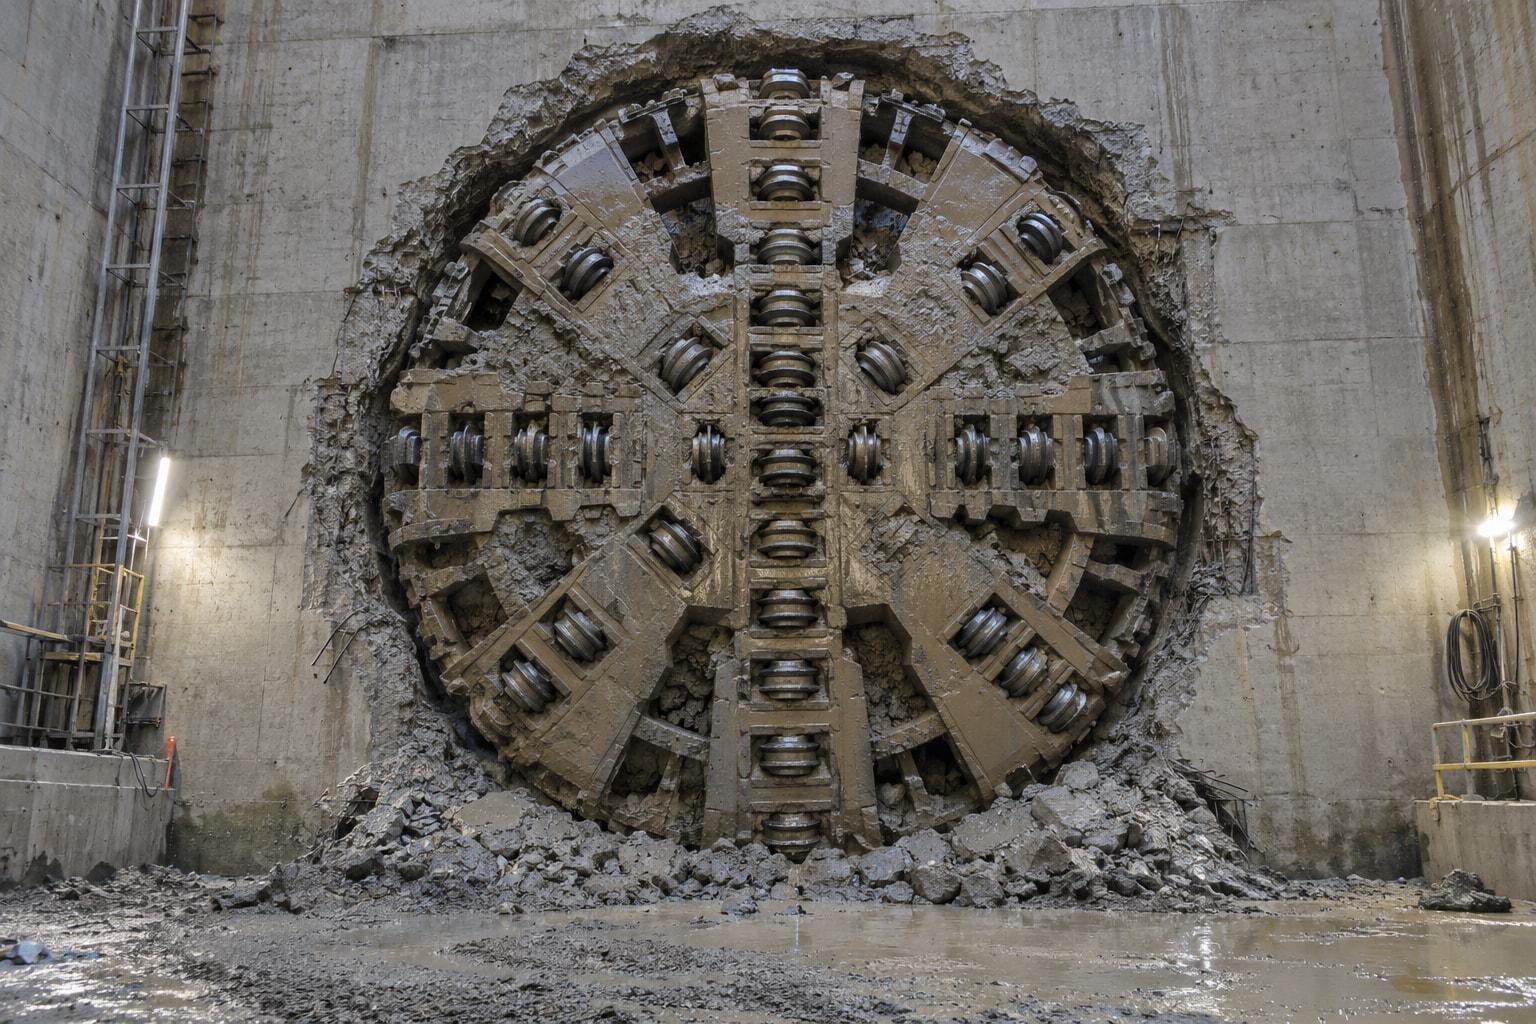
Slurry TBMs use pressurized bentonite slurry to support the tunnel face and carry excavated material to the surface. The BE-300 screens out coarse solids and uses cyclones to separate sand and silt, preparing the slurry for recirculation. When ground conditions introduce clay and finer silt, S3S adds centrifuges to control fine-solids buildup and maintain slurry performance.
Bentonite and polymer reuse
Recycling drilling slurry reduces fresh-fluid demand and liquid waste hauling. On drilled shaft work at the Gordie Howe International Bridge, polymer slurry recovery avoided disposal of approximately 160,000 gallons every two weeks. S3S dewaters spent slurry that cannot be reused into effluent and stackable solids, further reducing liquid disposal volumes.
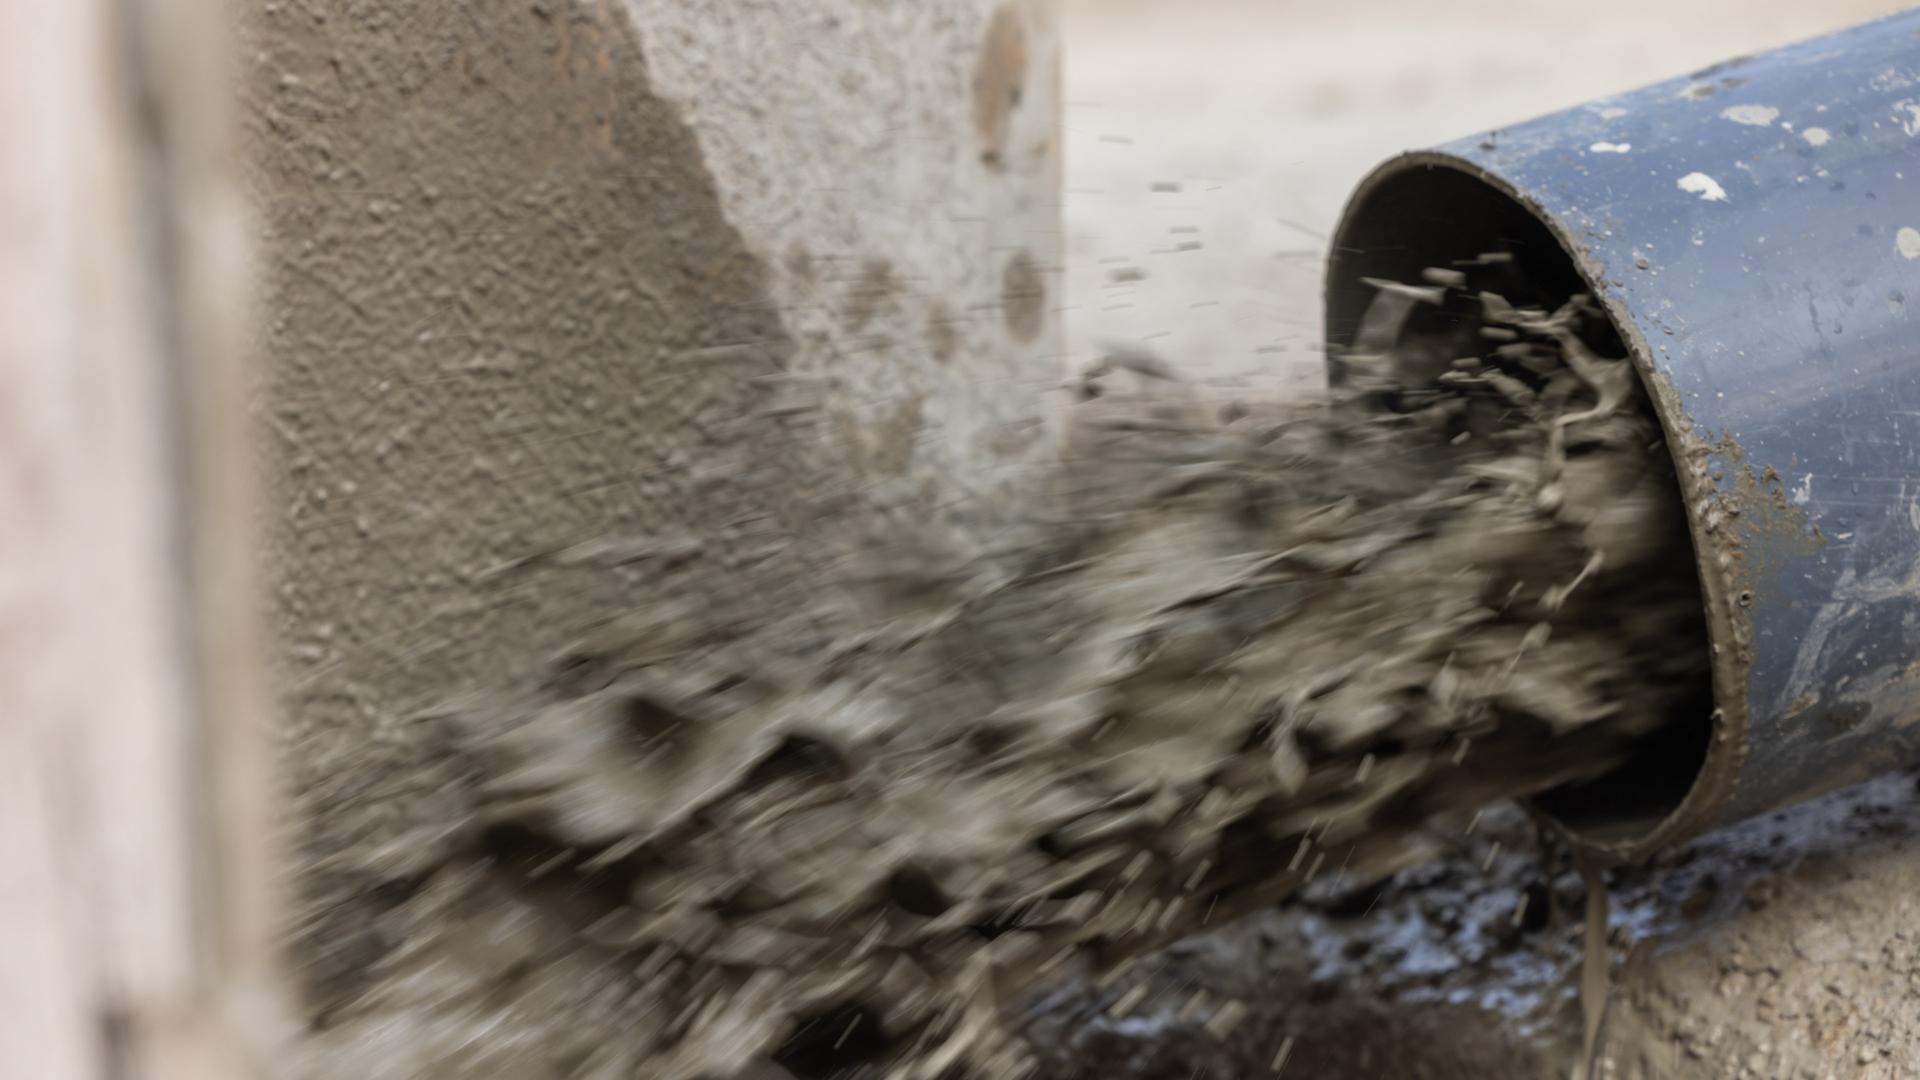
160,000 galPolymer slurry kept out of disposal every 2 weeks (drilled shafts, Gordie Howe International Bridge)
HDD
S3S processes returning HDD drilling fluid through shakers, cyclones, and centrifuges to remove drilled solids and return reusable mud to the rig. Controlling solids buildup helps maintain target mud weight, while dewatering produces stackable cuttings for efficient hauling and disposal.
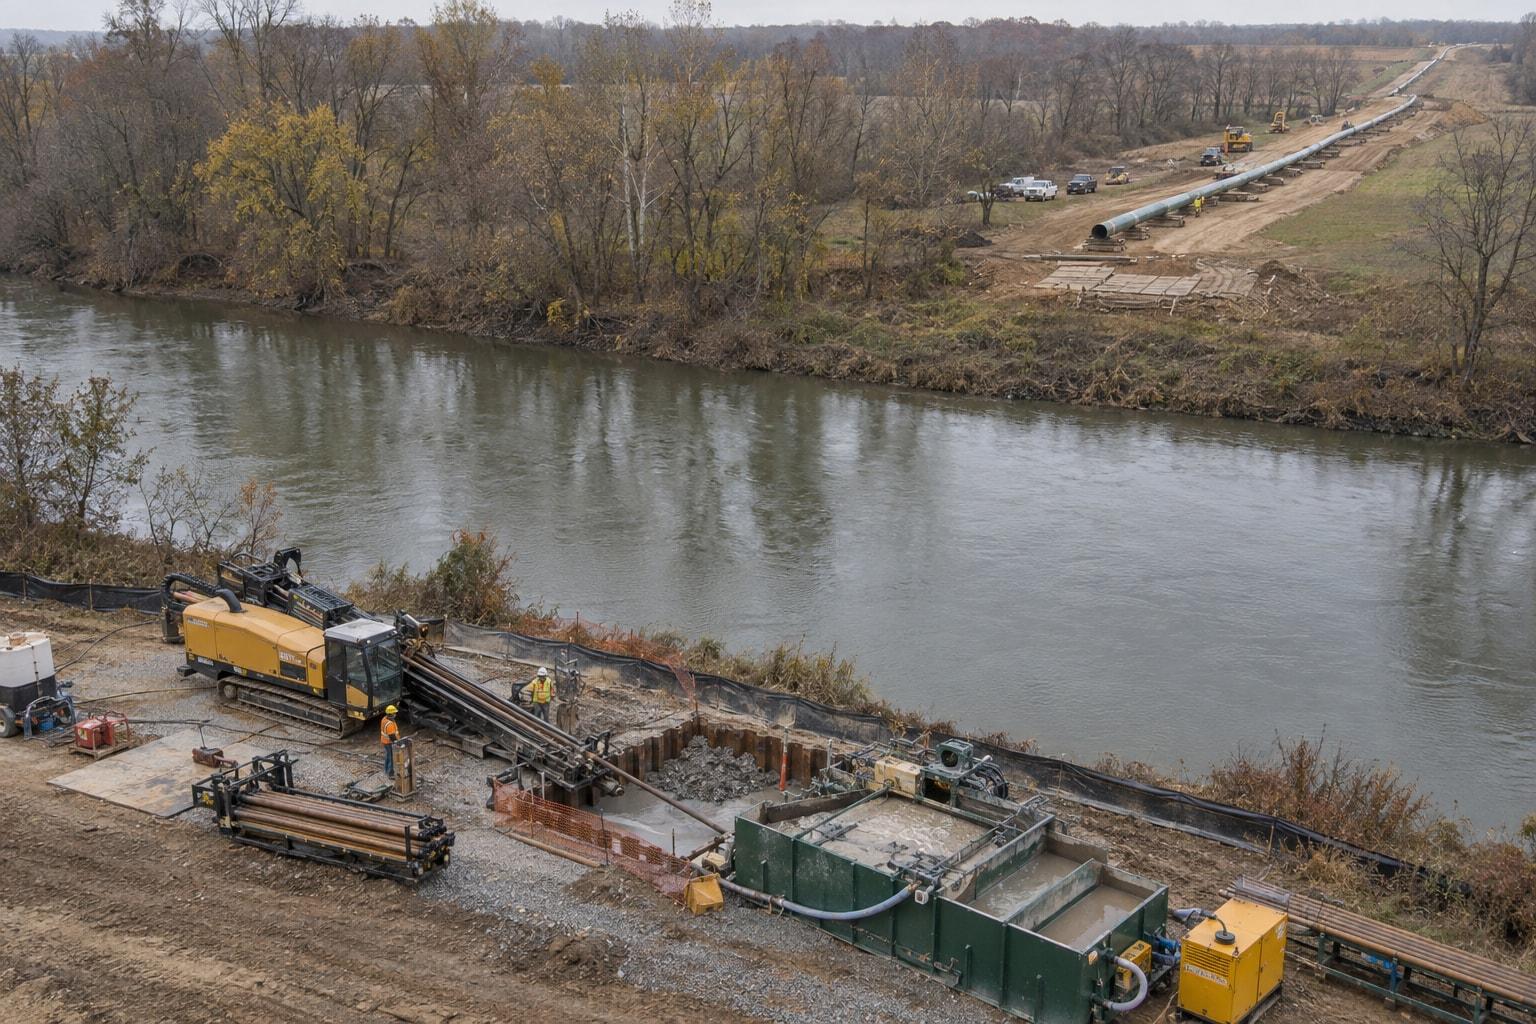
How we support your tunnelling or HDD project
We configure your separation plant around ground conditions, slurry flow, and site constraints to keep fluid circulating and excavation moving.
01
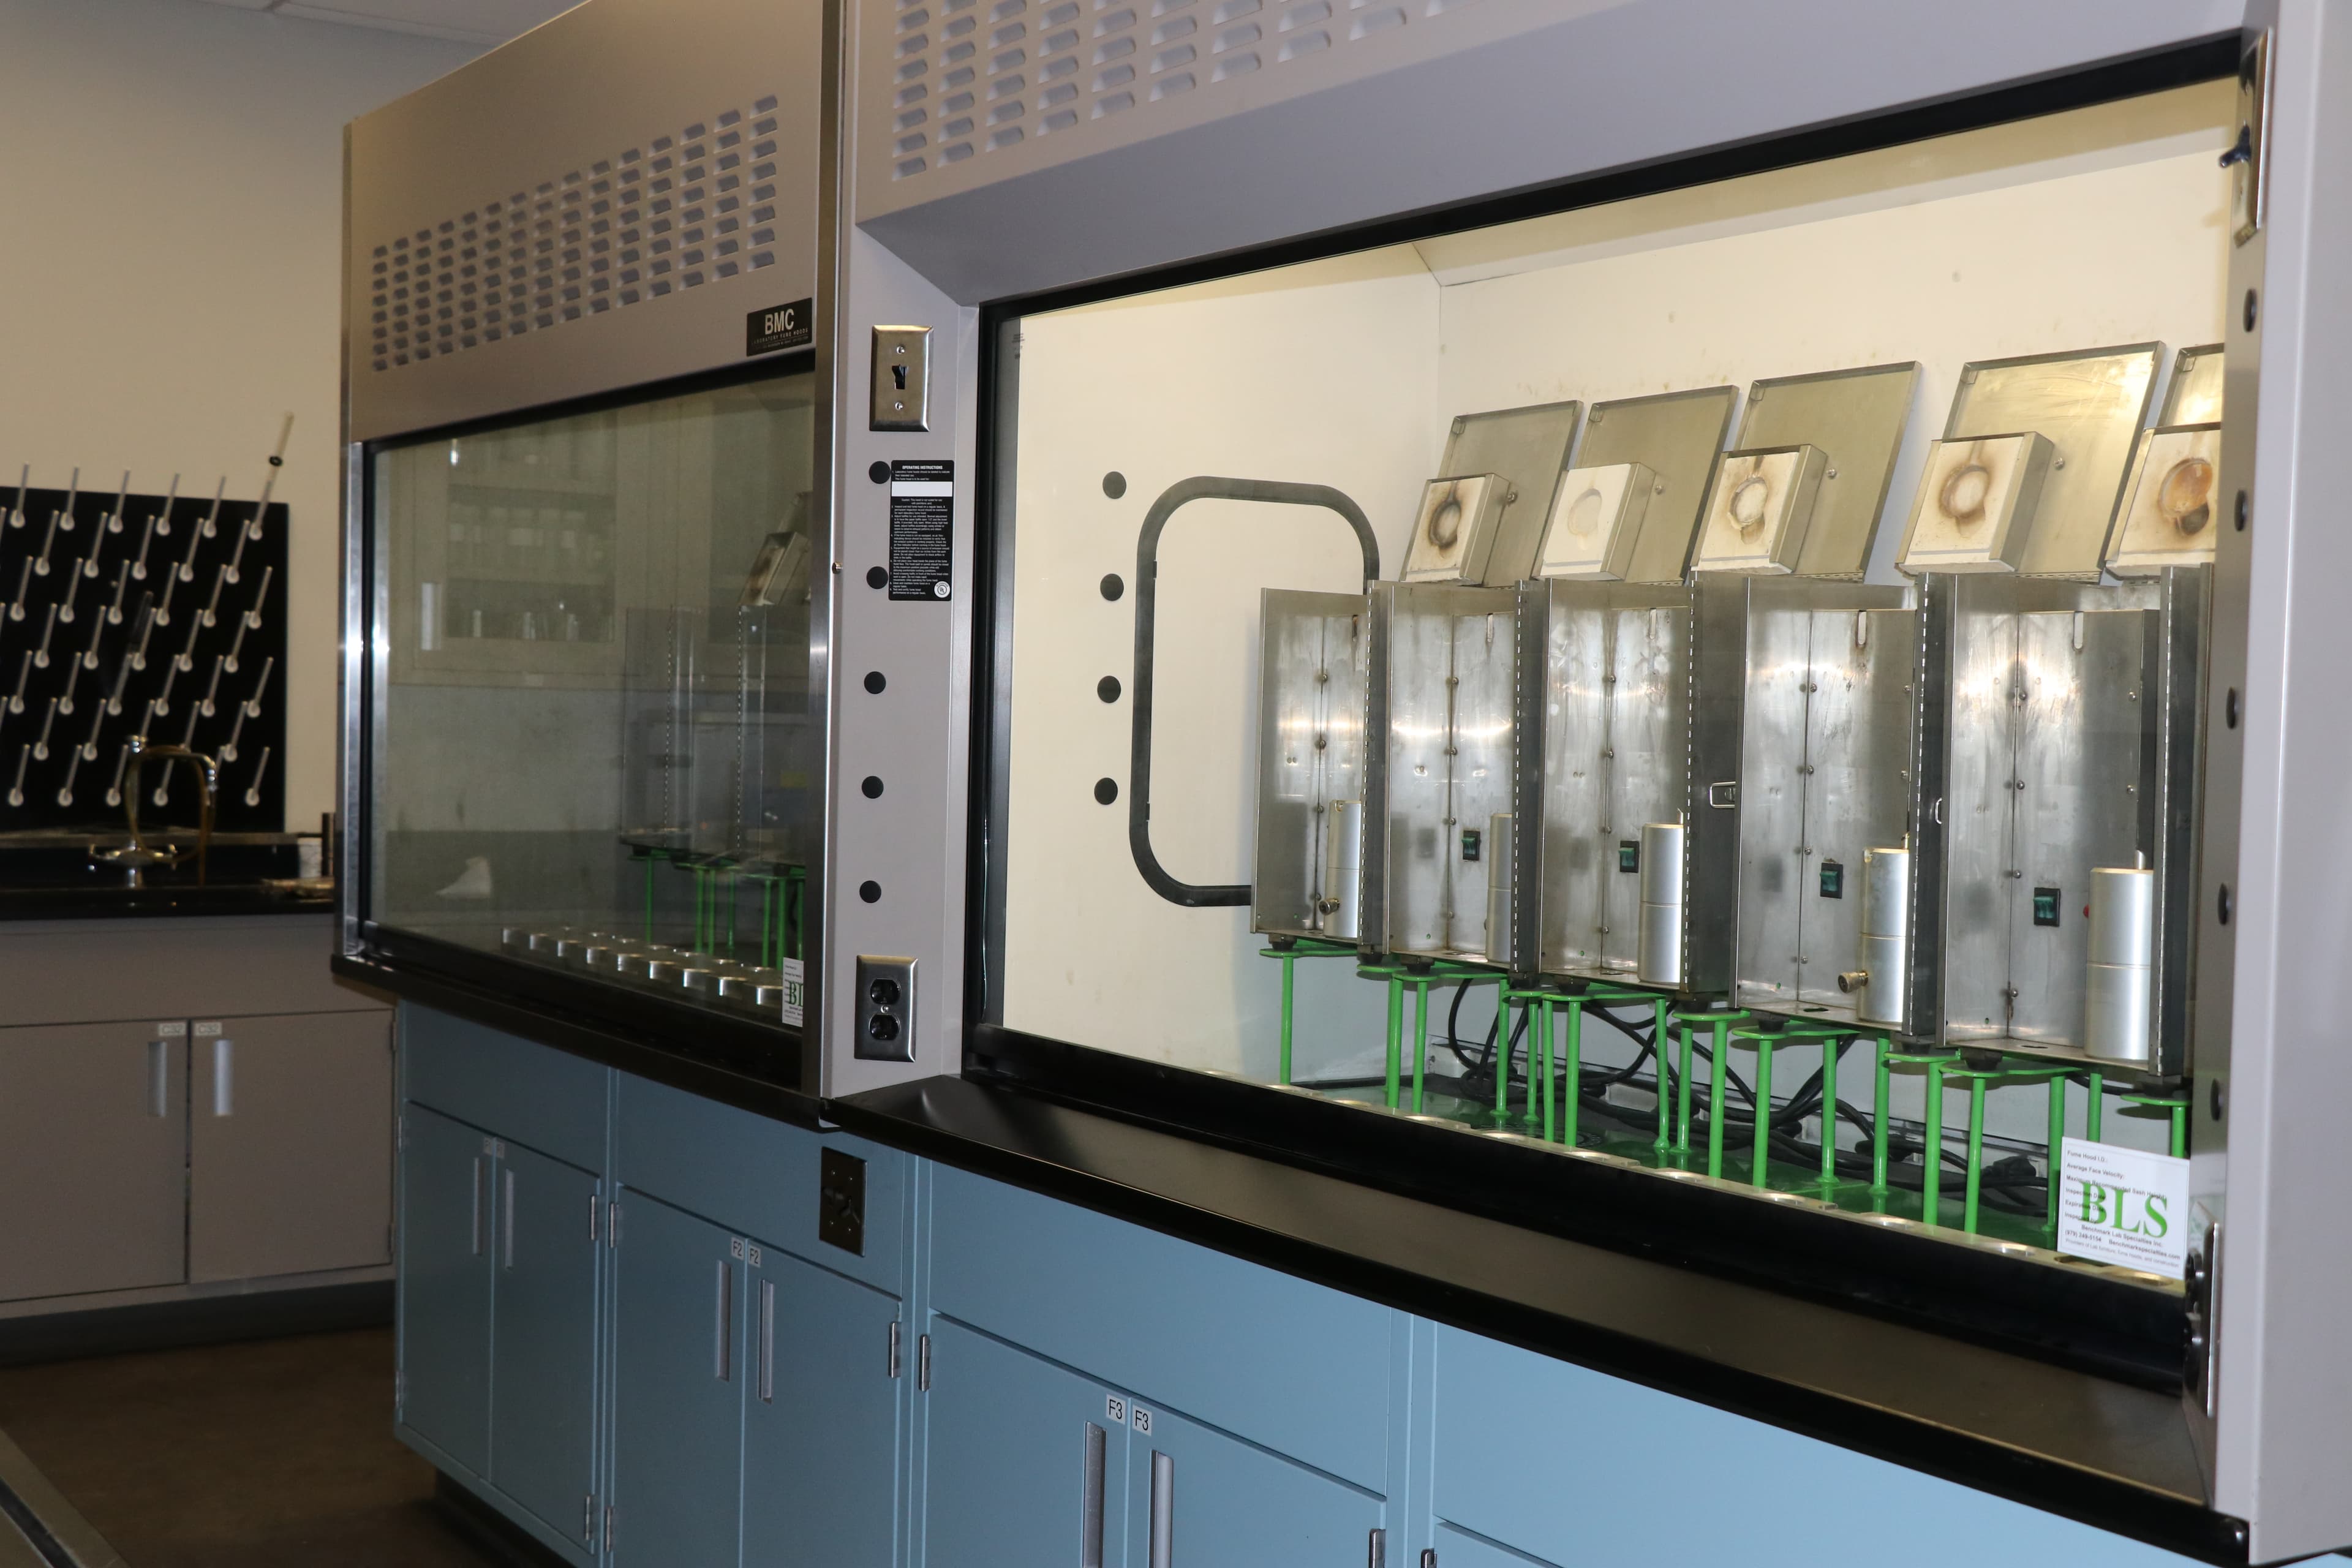
Match capacity to production
We size your plant around slurry flow and ground conditions, using lab testing where needed to define separation requirements.
02
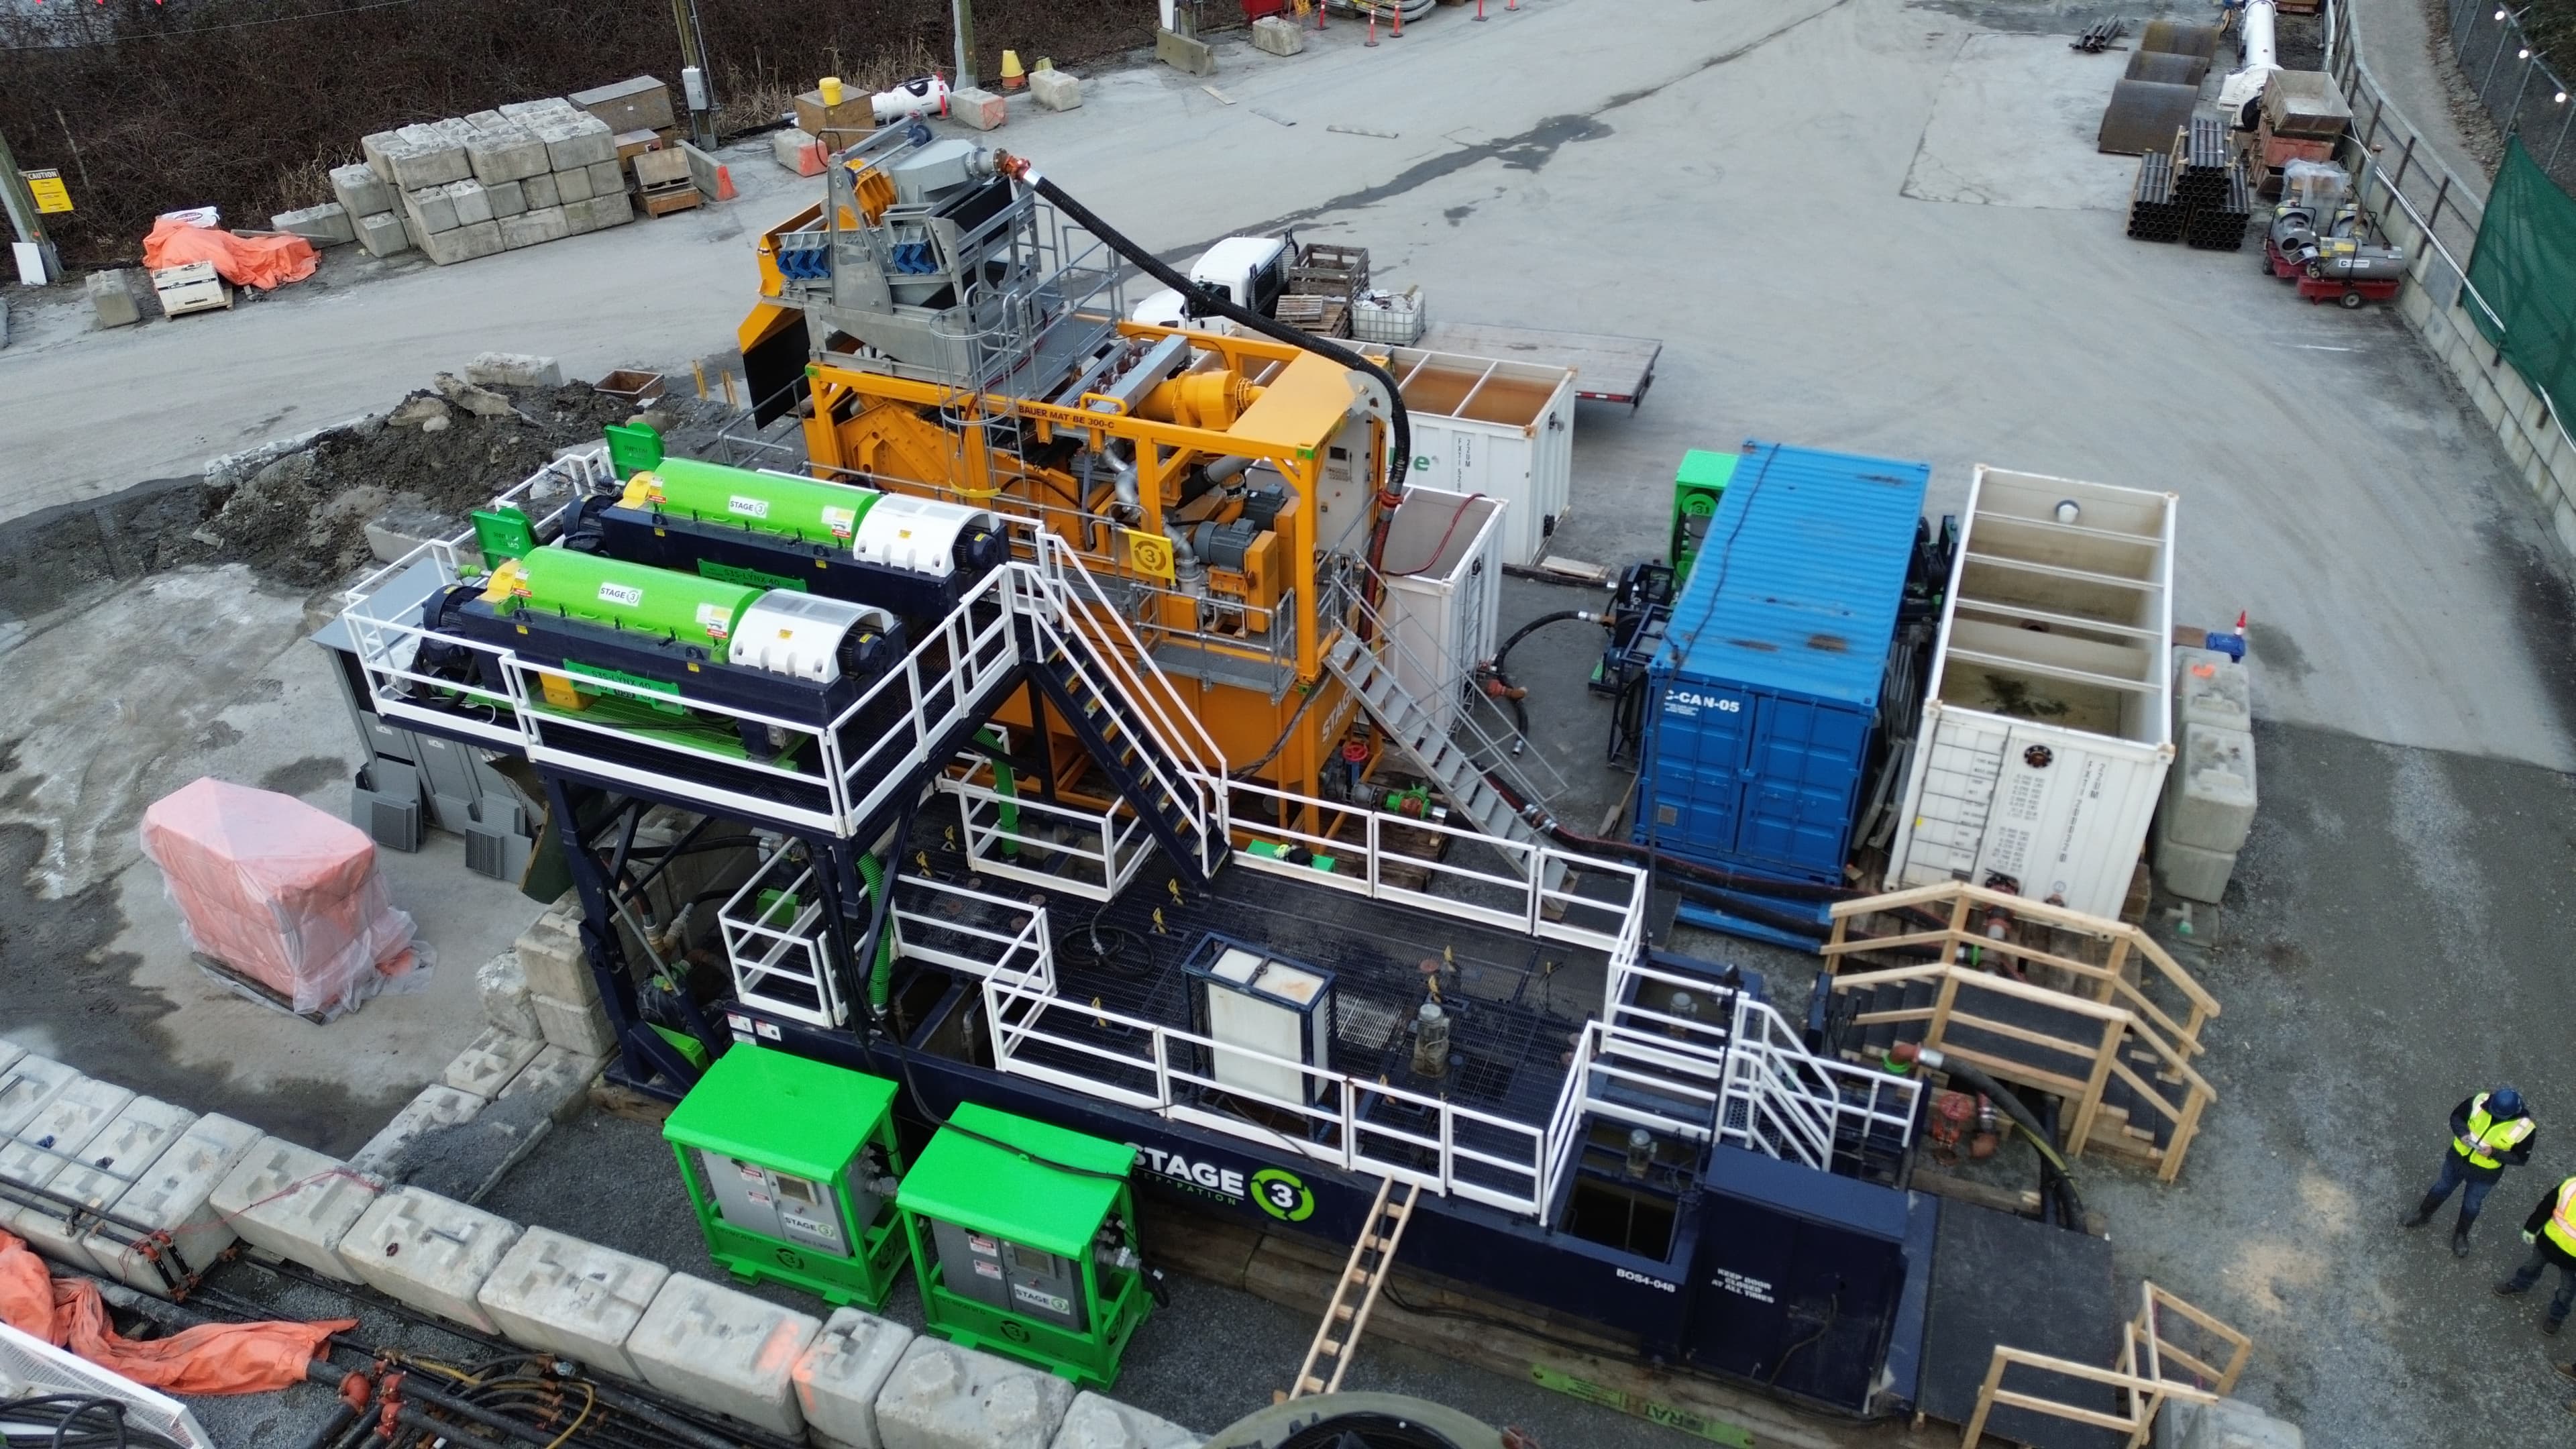
Set up
We design the layout around your shaft or work area, integrating screens, cyclones, tanks, and centrifuges into a complete separation system.
03
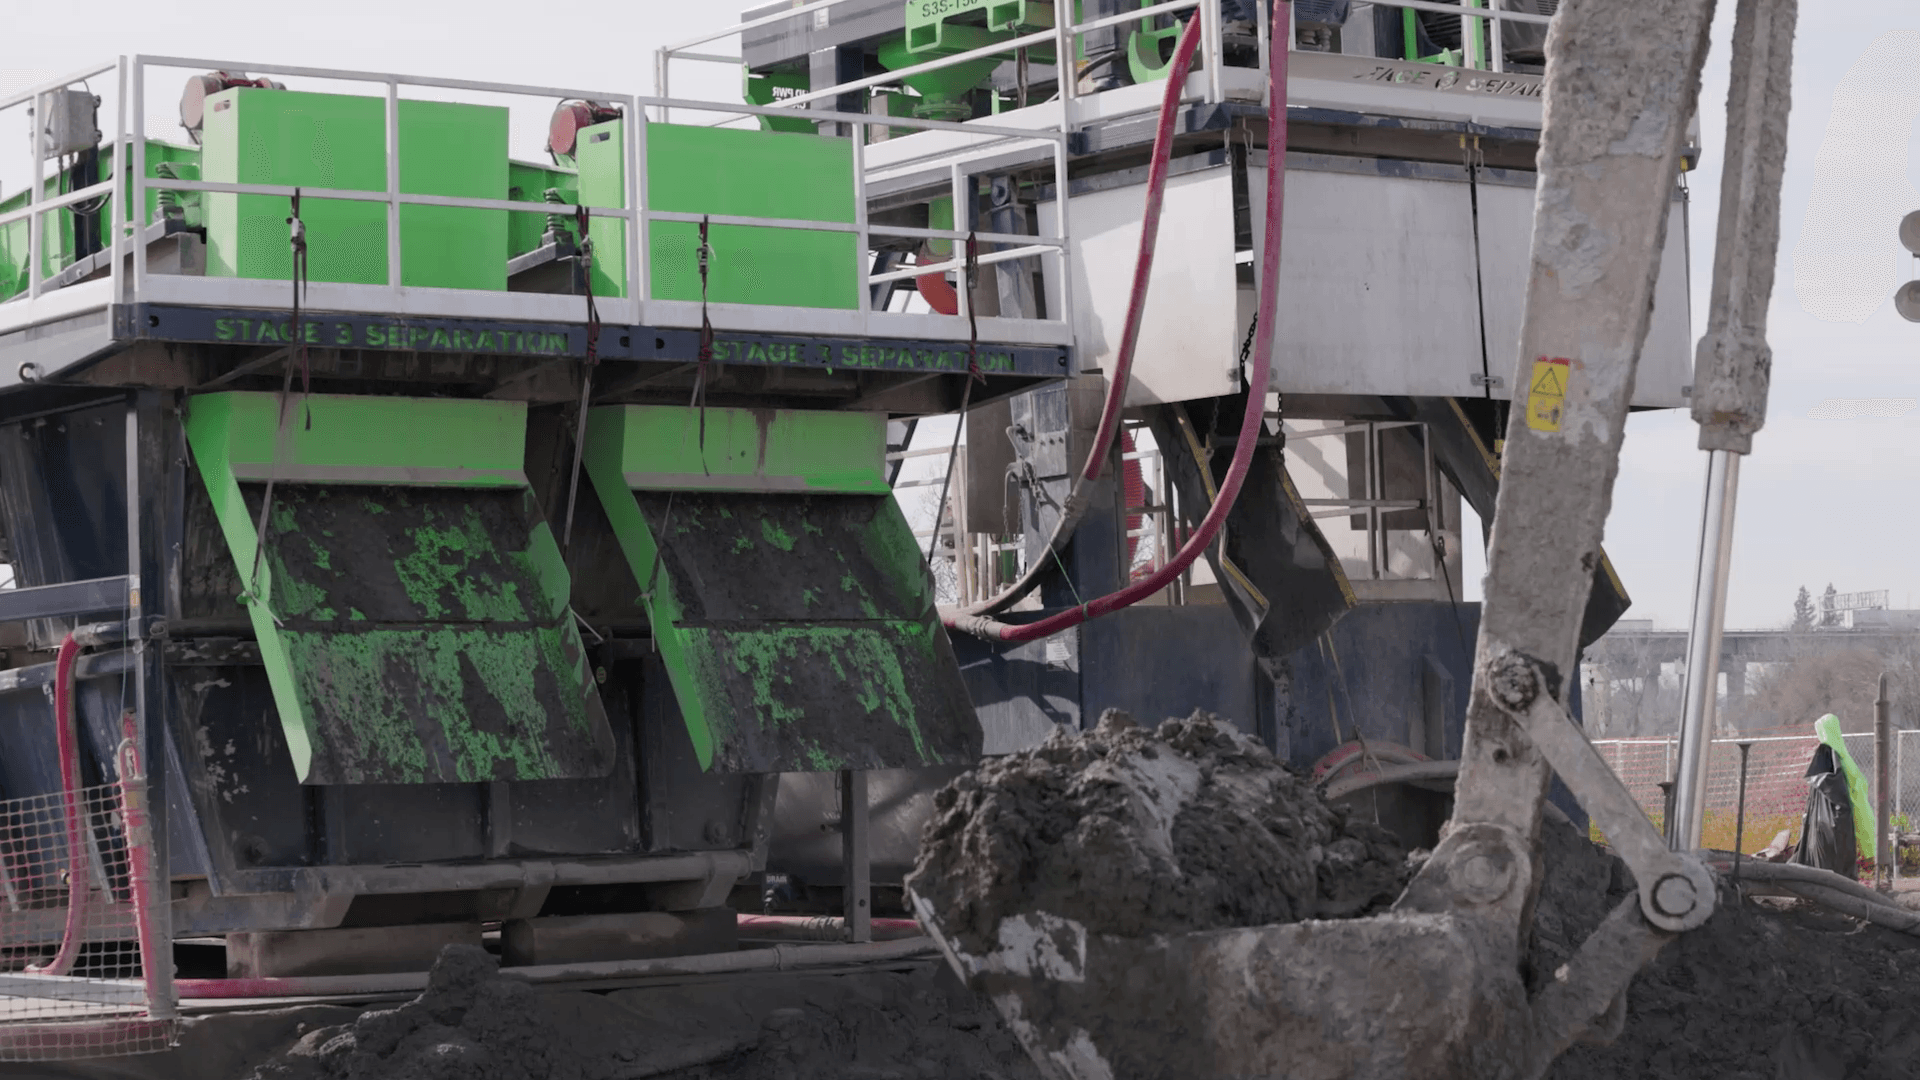
Separate
Technicians run the plant and test the slurry so it stays within your fluid targets.
Common questions from tunnelling and HDD contractors
Usually not. Earth pressure balance (EPB) machines hold the face with the excavated soil and remove it through a screw conveyor, so there is no slurry circuit to treat.
U.S. landfills generally require solids to pass the paint filter test: no free liquid draining within five minutes. Additives may require further testing, and acceptance depends on the landfill.
We can partner with you in numerous ways. Most jobs run with S3S technicians. If your crew wants to run the equipment, we can train them first.
Talk to an equipment specialist about your tunnel or bore
Share your drilling method, slurry flow, ground conditions, and available space so we can configure the right separation system.
What happens next
- An equipment specialist reviews the details with you.
- We size the plant and crew.
- You get a scope you can price.